Moisture-Proof Cabinet: The Ultimate OEM-Guided Solution for Protecting Electronics, Sensitive Parts, and Valuable Inventory
Learn how industrial-grade moisture-proof cabinets eliminate 99% of humidity-related damage to electronics, precision components, and collectibles, with custom OEM options tailored to your unique storage requirements.
- What Exactly Is a Moisture-Proof Cabinet, and How Does It Work?
- Core Standard Features of Our Manufacturer-Direct Units
- The Most Common Humidity-Related Problems a Moisture-Proof Cabinet Solves
- Custom OEM Options From Our Direct Manufacturer
- Popular Customization Options
- Key Takeaways
- Frequently Asked Questions
- What RH level should I set my moisture-proof cabinet to for electronics storage?
- Can I order a custom color or branded exterior skin for my OEM moisture-proof cabinet?
- How long do industrial moisture-proof cabinets last with regular use?
- Do moisture-proof cabinets require a dedicated water drain line?
If you work with sensitive electronics, semiconductor wafers, camera gear, 3D printed resin parts, or high-value inventory, you already know that unregulated humidity causes an estimated 30% of all unplanned product failures in manufacturing and storage environments, per global electronics industry testing. A high-quality moisture-proof cabinet is purpose-built to maintain stable relative humidity (RH) levels between 1% RH and 50% RH, eliminating corrosion, mold, delamination, and water damage that ruins valuable assets. As a leading manufacturer of professional dry storage solutions, we offer fully customizable OEM options, including custom exterior skin finishes, size configurations, and access controls to match your exact operational needs.
What Exactly Is a Moisture-Proof Cabinet, and How Does It Work?
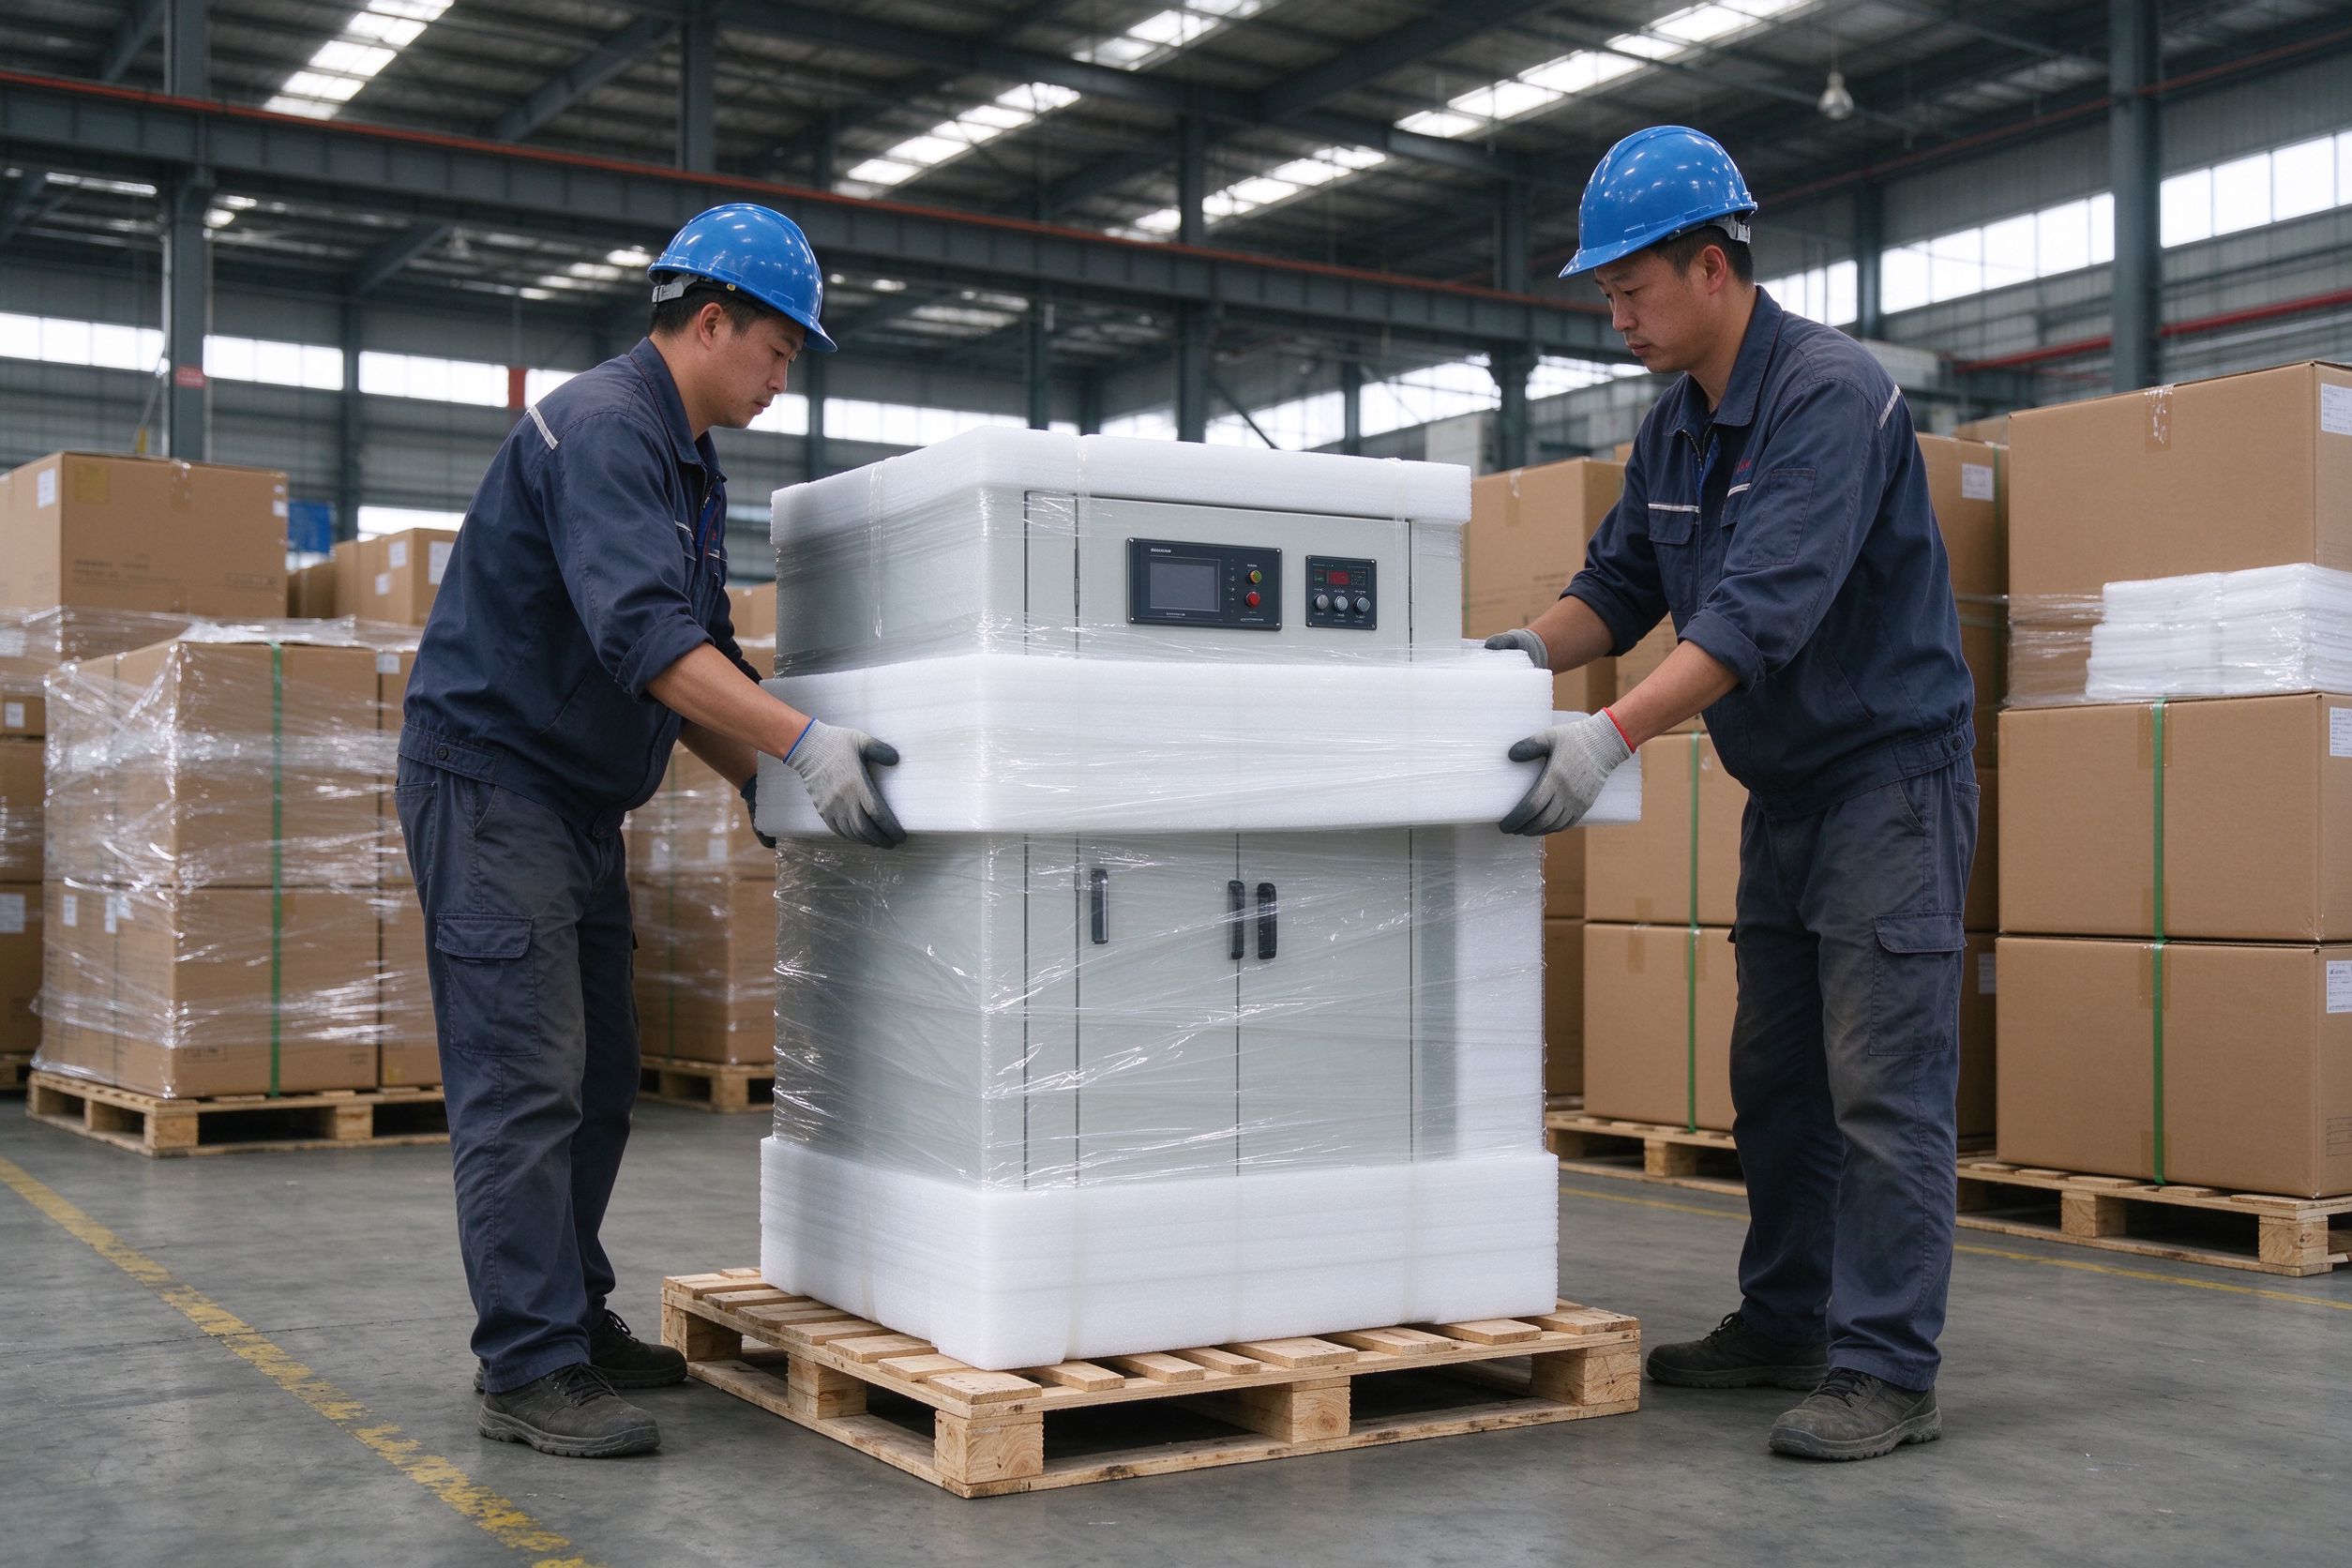
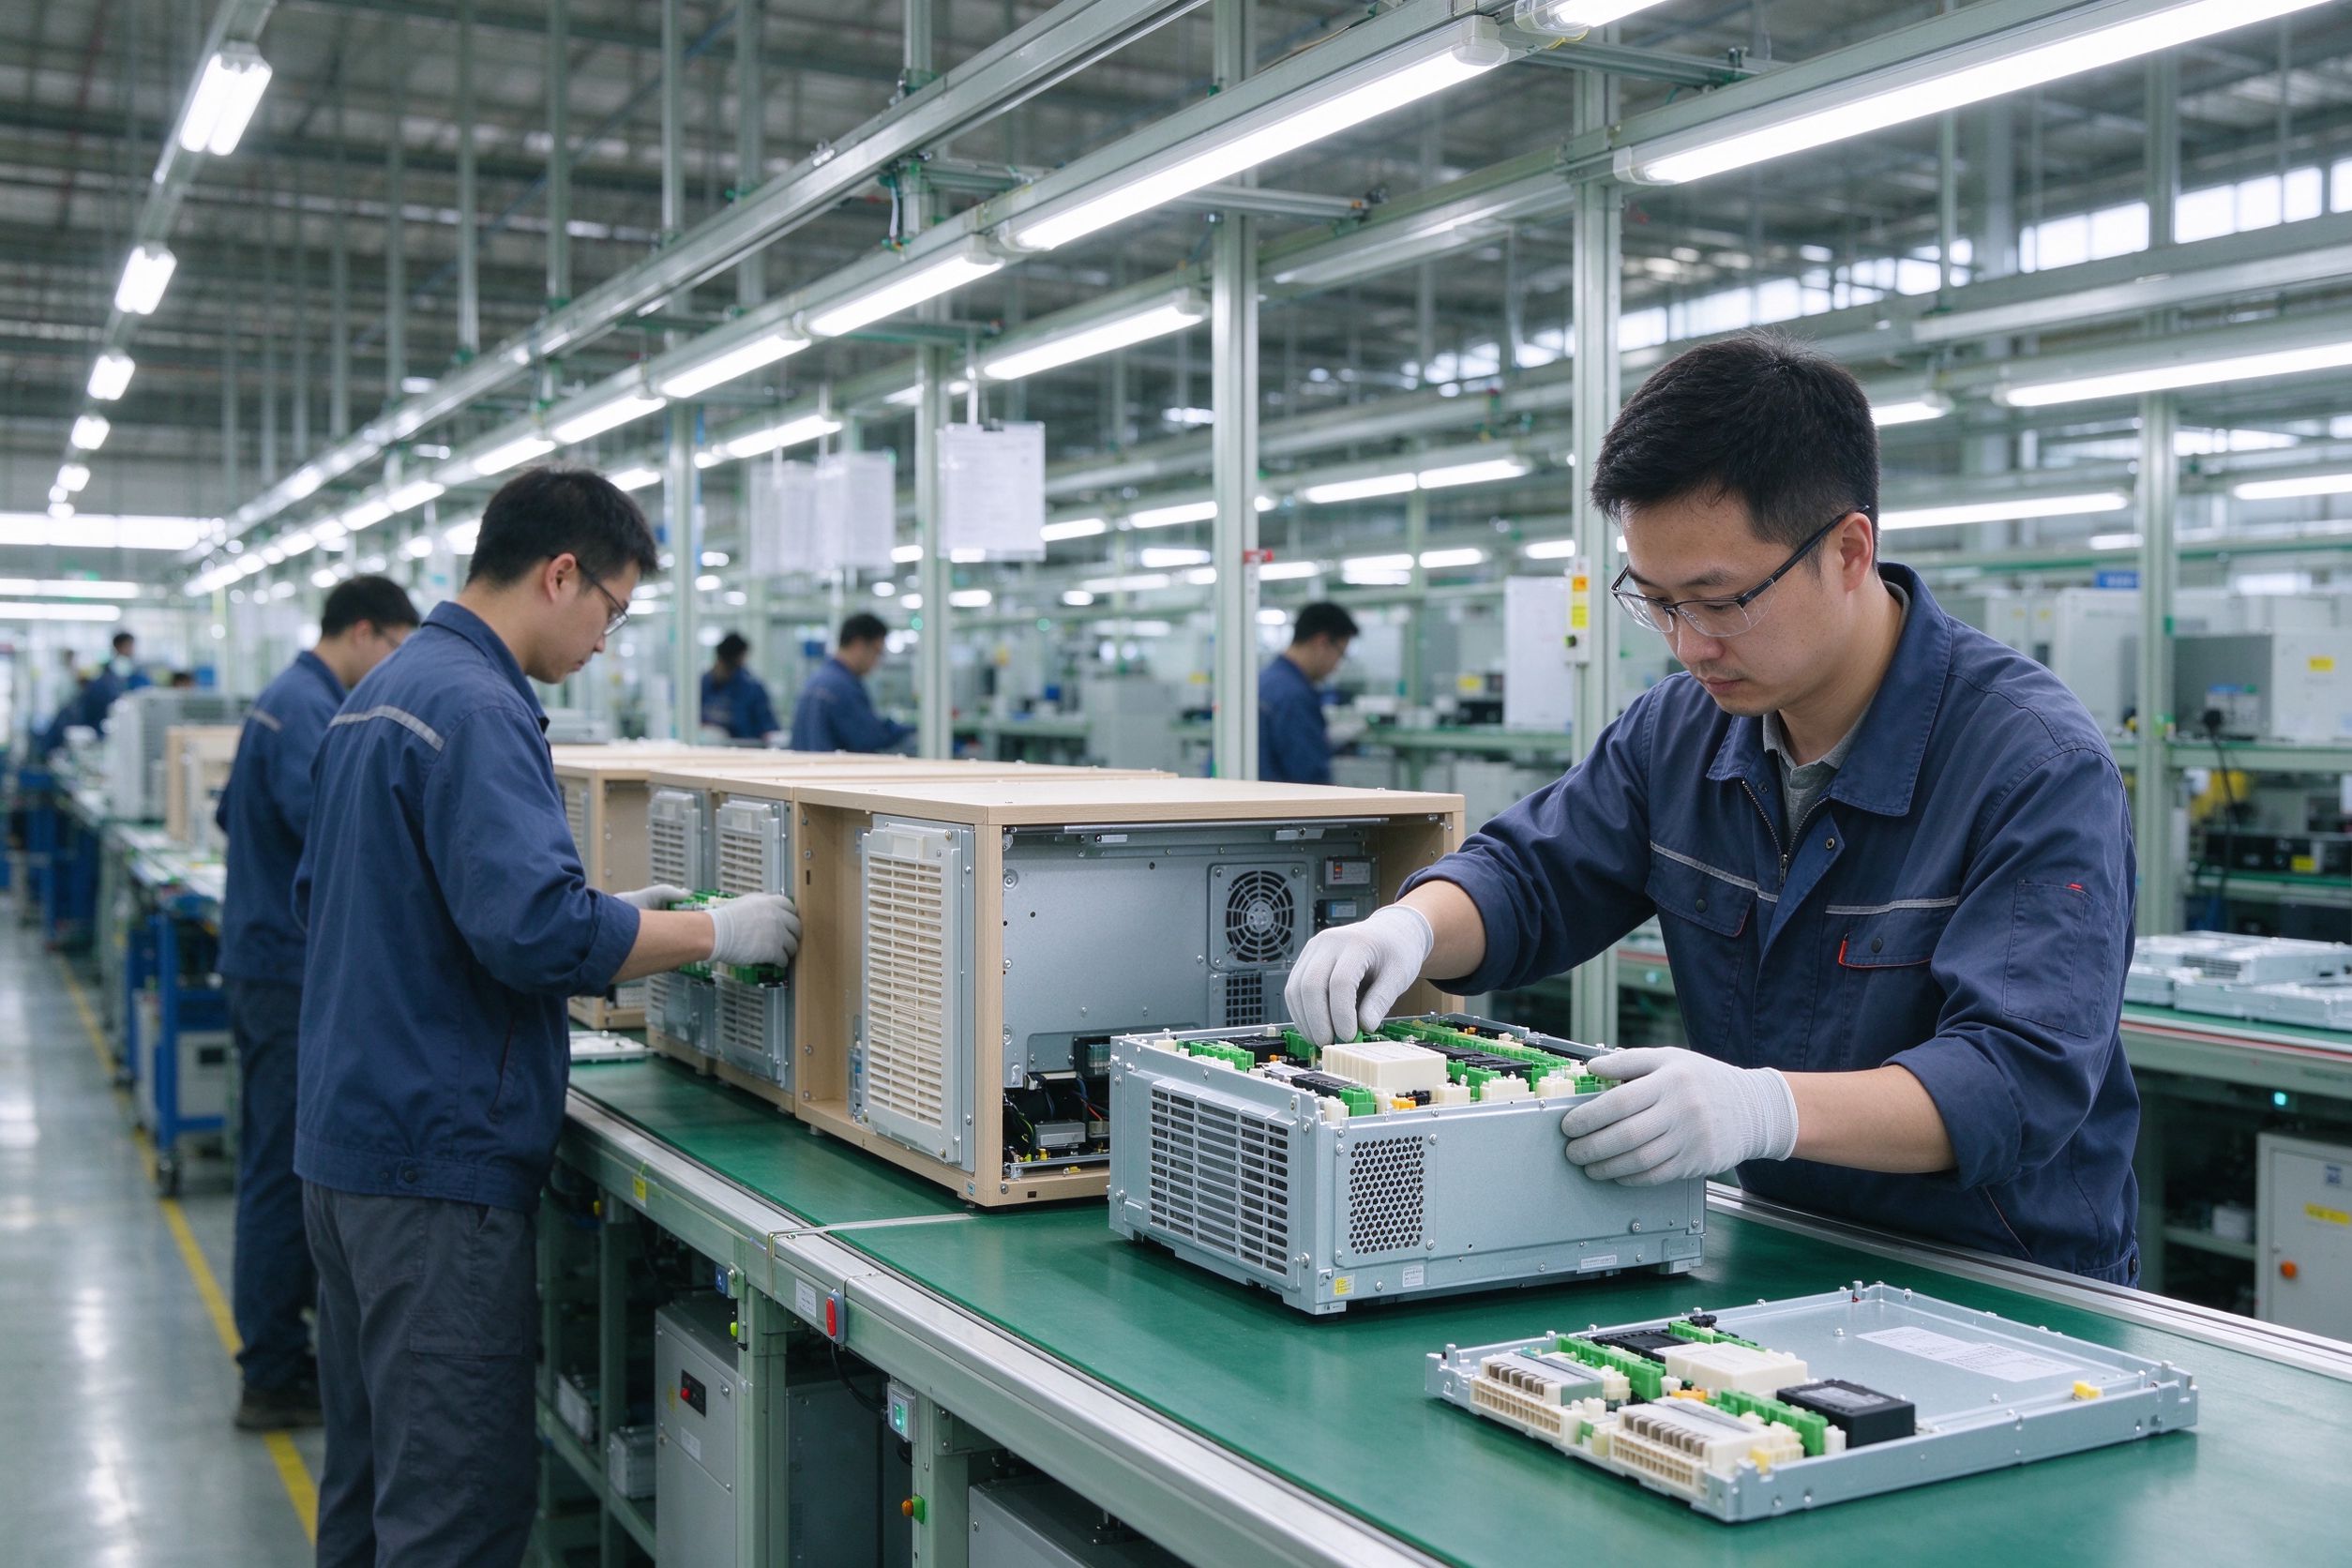
Unlike basic kitchen storage cabinets or generic plastic seal boxes, industrial moisture-proof cabinets use a combination of sealed, reinforced construction, low-power dehumidification modules, and precision RH sensors to maintain consistent low-humidity environments 24/7, no desiccant replacement required for up to 10 years of regular use.
Core Standard Features of Our Manufacturer-Direct Units
- Airtight silicone-sealed door frame that reduces ambient moisture ingress by 97% compared to standard cabinet doors
- Digital RH and temperature display with ±2% RH accuracy for real-time monitoring
- Adjustable shelf load capacity up to 150kg per tier for heavy industrial components
- Optional anti-static ESD coating for safe storage of electrostatic-sensitive circuit boards
The Most Common Humidity-Related Problems a Moisture-Proof Cabinet Solves
Without proper dry storage, even small fluctuations above 60% RH can trigger irreversible damage to high-value items in weeks or even days.
- Corrosion on copper and metal connector pins that causes 42% of circuit board failures in unused inventory
- Delamination of camera lens coatings and fogging on precision optical equipment
- Caking and clumping of 3D printing resin powder, pharmaceutical raw materials, and specialty chemicals
- Mold growth on vintage paper documents, leather goods, and collectible electronics
Custom OEM Options From Our Direct Manufacturer
Unlike off-the-shelf moisture-proof cabinets that force you to adapt your workflow to a pre-set size and design, our in-house manufacturing team delivers fully customized OEM solutions tailored to your use case, with no minimum order quantity for small-batch custom requests for qualified business customers.
Popular Customization Options
- Custom exterior skin finishes: Choose from powder-coated steel in 20+ RAL colors, stainless steel 304/316 skins for cleanroom environments, or scratch-resistant textured skins for heavy factory floor use
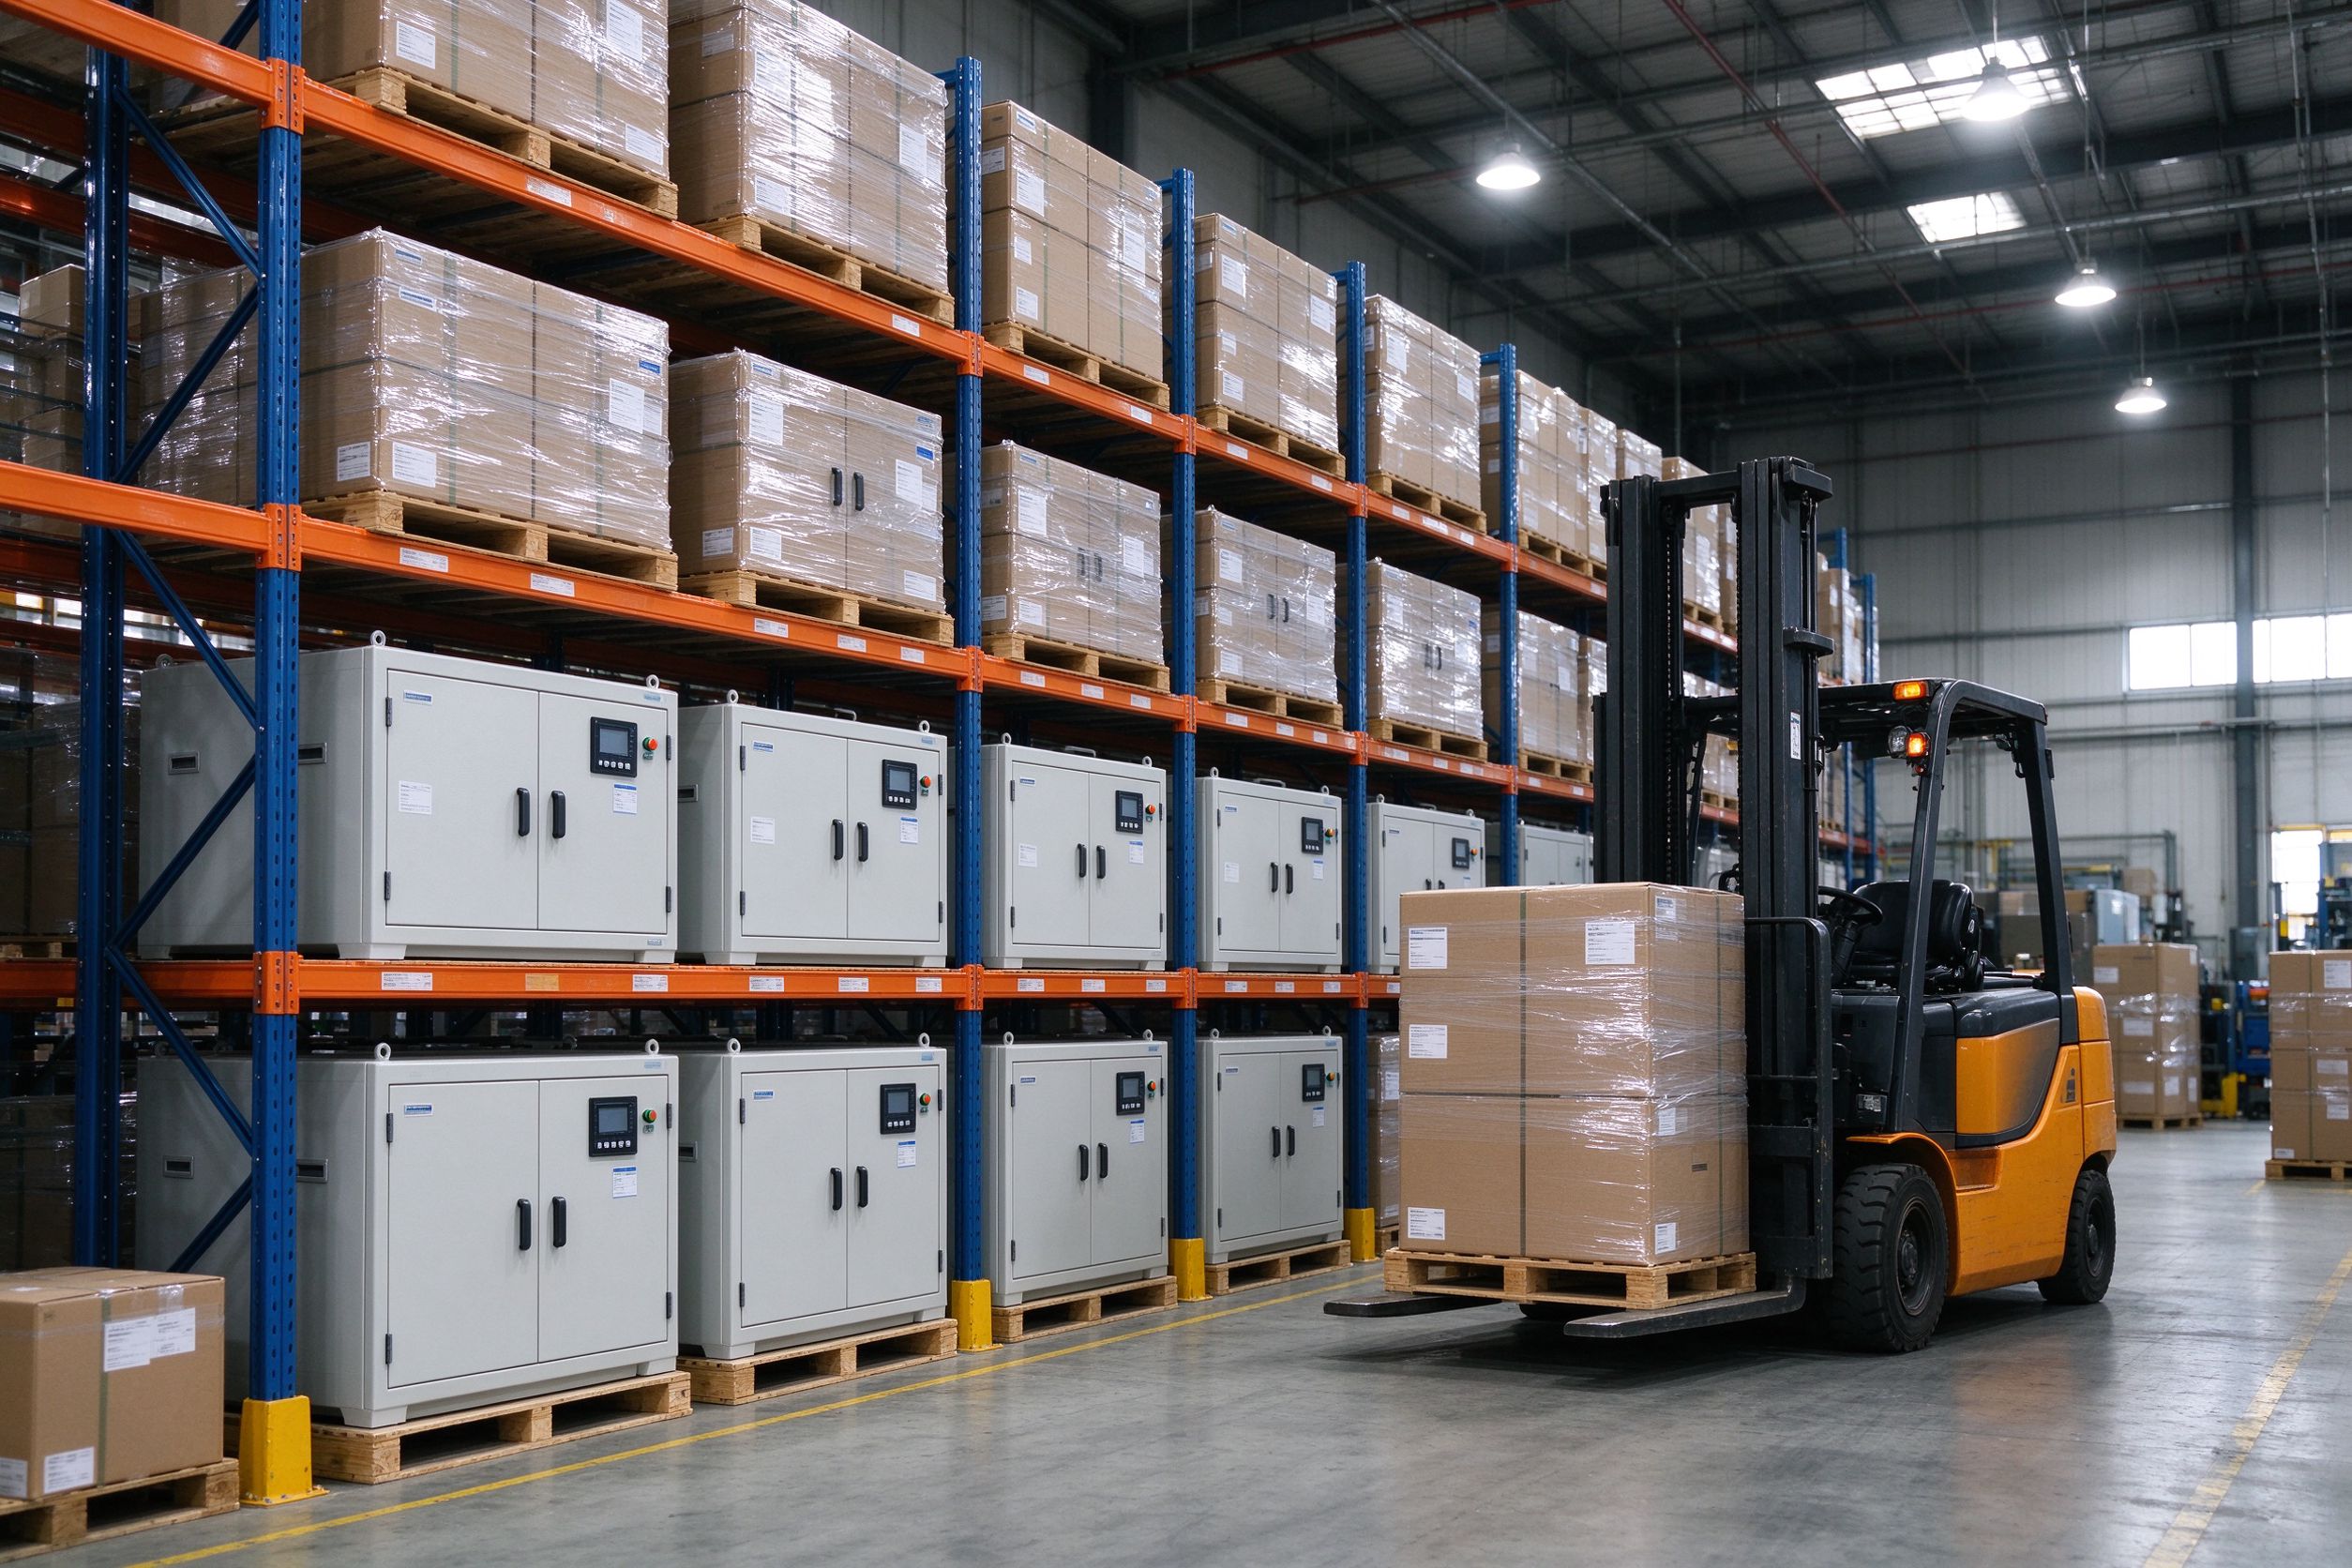
- Custom dimension adjustments: Build units as narrow as 30cm for lab benchtops, or as tall as 2.5m for warehouse bulk storage
- Special function upgrades: Add biometric access locks, remote WiFi RH monitoring, nitrogen purge ports, or built-in UV disinfection modules
- Branding customization: Print your company logo, custom warning labels, or user instruction guides directly on the cabinet skin for seamless brand integration
Key Takeaways
- A high-quality moisture-proof cabinet reduces humidity-related product loss by up to 99% for electronics, precision parts, and valuable inventory
- Standard units maintain stable RH levels between 1% and 50% RH with no regular desiccant replacement for 10+ years of operation
- Our manufacturer-direct OEM program lets you customize exterior skin finishes, dimensions, and functional features to match your exact operational requirements
- Industrial-grade units support shelf load capacities up to 150kg per tier, suitable for both small lab and large warehouse use cases
Frequently Asked Questions
What RH level should I set my moisture-proof cabinet to for electronics storage?
For most consumer and industrial electronics, set your cabinet to 30% to 40% RH to eliminate corrosion risk without drying out rubber seals or plastic components. For semiconductor wafer storage, use a 10% RH ultra-low humidity setting.
Can I order a custom color or branded exterior skin for my OEM moisture-proof cabinet?
Yes, our manufacturing team offers 20+ standard RAL color powder coat skins, custom stainless steel skins, and full custom branding printing on all cabinet exteriors for OEM orders of any size.
How long do industrial moisture-proof cabinets last with regular use?
With basic annual filter cleaning, our units have a service life of 12 to 15 years, with no consumable parts required for the dehumidification system.
Do moisture-proof cabinets require a dedicated water drain line?
No, all our electric dehumidification modules use a heat regeneration system that releases absorbed moisture directly back into ambient air, no drain line or water collection bucket required.